Home  /  On-site resources

On-site equipment and process capability.

Equipment, utilities, storage and logistics available within the classified space. All items listed are installed and in production use. Shared resources are included with a space engagement. Requirements not listed are identified during scoping and either sourced or specified as customer-supplied.

Equipment not listed can frequently be sourced faster than customer procurement.
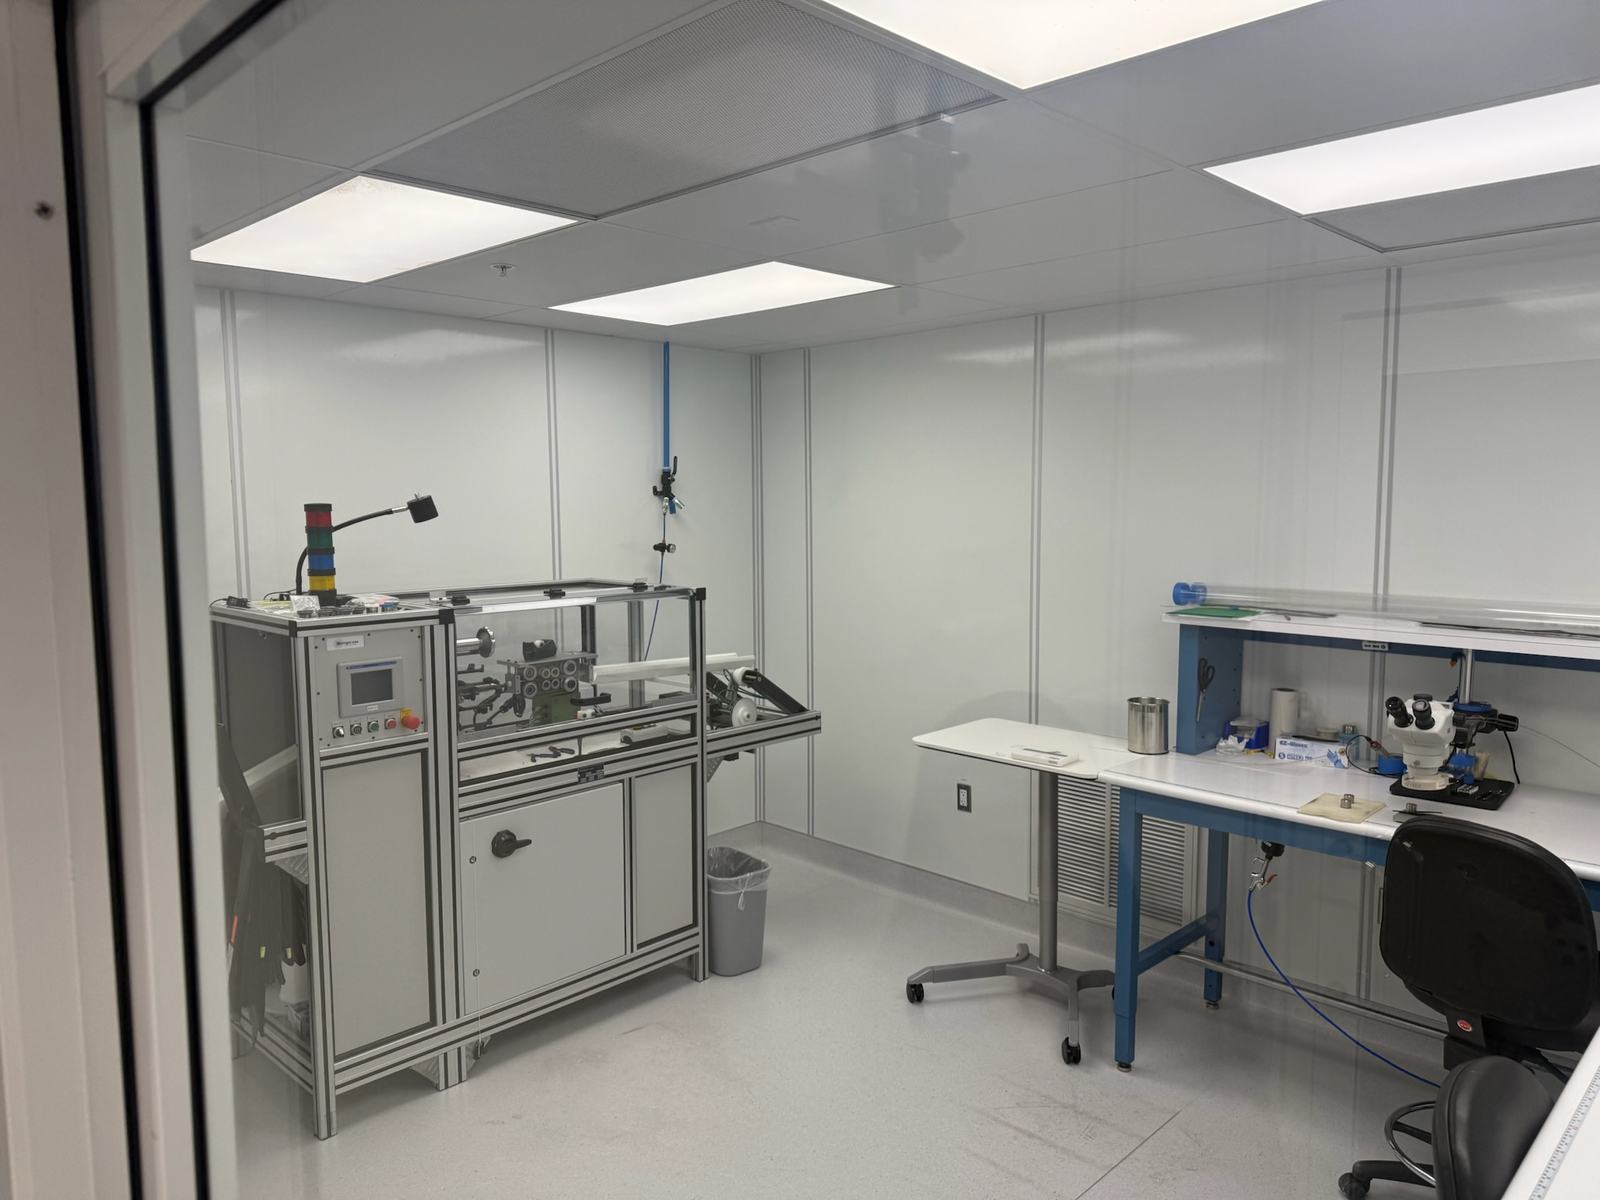
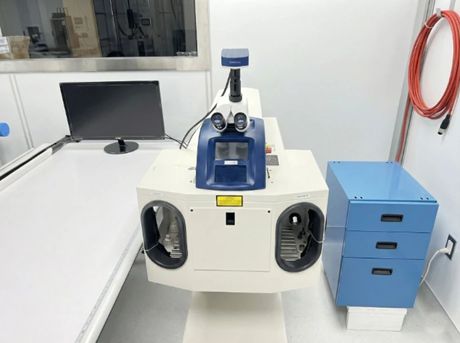
Process equipment and an ESD bench with stereo microscope inside the MedTech Innovation cleanroom
Included
Shared equipmentWith any space engagement
Utilities
Clean dry airFiltered and plumbed to every bench
Logistics
Ship aheadReceived, logged and staged
People
Ours or yoursTechnicians and senior engineering
Process & assembly Packaging & verification Facility utilities Storage & shipping People What to bring

01 / At the bench

Process & assembly

Installed and running

Assembly equipment within the classified space. No process step requires removal from the cleanroom.

ResourceWhat it doesNotes
UV curing stationsSpot cure of UV adhesives at bond joints — tip bonds, hub bonds, strain reliefs, marker bands.Spot cure
UV assembly & curing fixturesHold geometry while the joint cures, so bond position and concentricity repeat unit to unit.Program-specific
EFD dispensersControlled, repeatable adhesive placement by volume and time instead of by hand feel.Benchtop
Stereo microscopesAssembly, bonding and in-process inspection at the bench.6×
Lamination & reflow ovenLarge-format oven for lamination, reflow and coating cure across full working-length assemblies — controlled, uniform thermal profile over the whole device.Oven
Batch processing ovenThermal cure, anneal and reflow steps run as controlled batches.Batch
Ultrasonic cleanerComponent cleaning before assembly and between process steps.Benchtop
ESD workbenchesStatic-safe assembly surfaces with overhead lighting, power and air at each station.Dedicated
Hot air systemsLocalized heat for shrink, reflow and forming operations.At bench
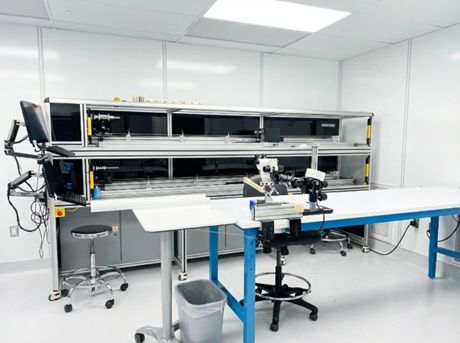
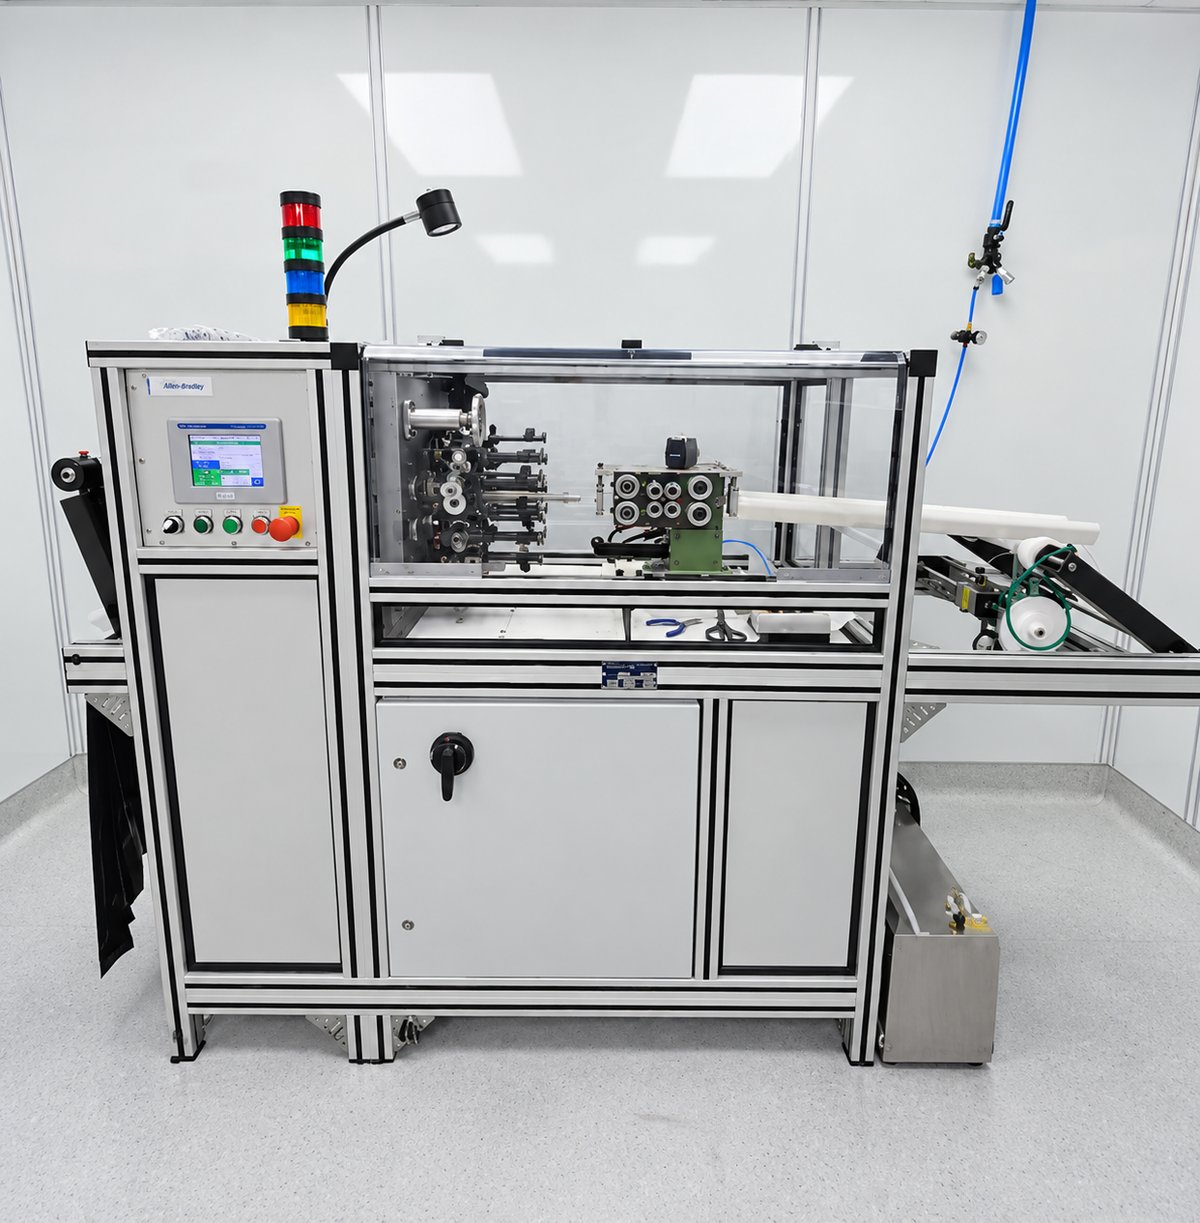
Automated braiderProgrammable braiding for braid-reinforced shaft constructions — controlled pick count, wire size and pattern across the working length.Automated
Automated braiding machine with Allen-Bradley touchscreen controller and catheter mandrel
Automated braiderProgrammable braiding for braid-reinforced shaft constructions.
Automated laser inspection system on a dedicated instrument base
Laser Equipment
Coil winder and coil inspection table in the cleanroom
Coil Winder and Coil Inspection Table
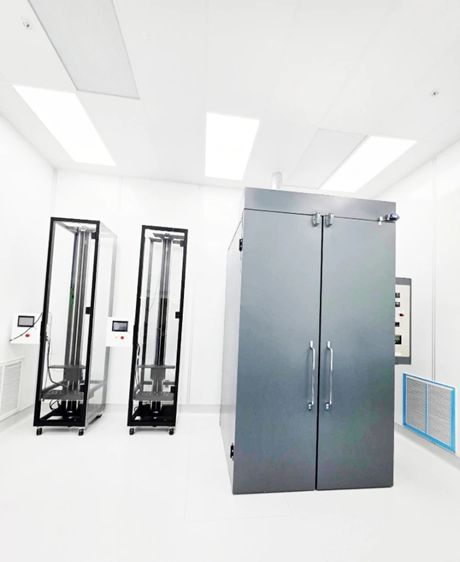
Hydrophilic coating towers beside a large stainless double-door lamination and reflow oven in the cleanroom
Dip Coating Machine and Large-Format Oven Coating Cure

02 / Sealed and checked

Packaging & verification

Inside the classified space

Packaging is performed in the classified space. The sterile barrier is applied before the device is exposed to uncontrolled air.

ResourceWhat it doesNotes
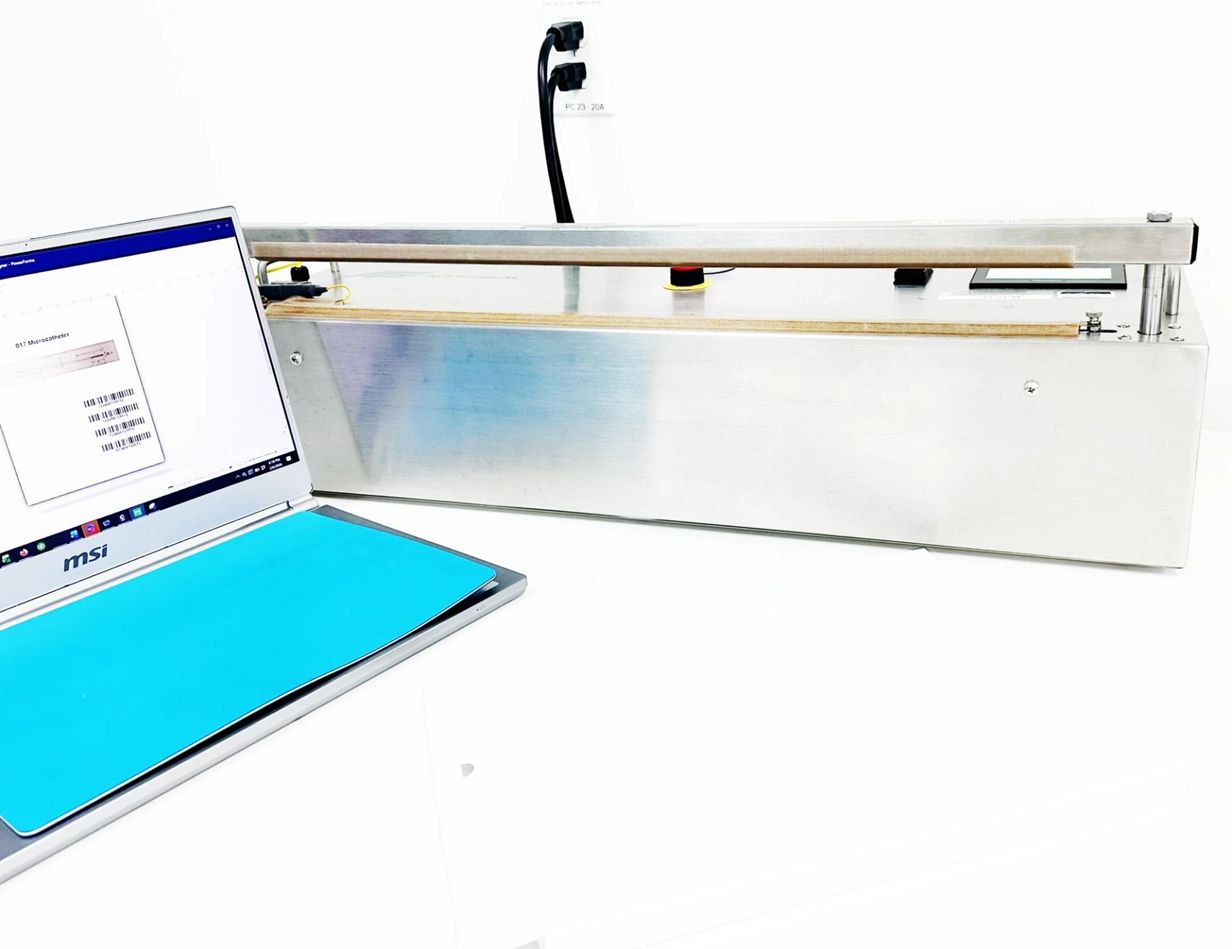
Pouch sealerSeals sterile barrier packaging inside the cleanroom, so packaging is not a re-contamination step.In-room
Seal peel testerVerifies seal strength and integrity on the packaging you just produced.12"
Leak testerLumen and joint integrity checks on finished and in-process assemblies.Benchtop
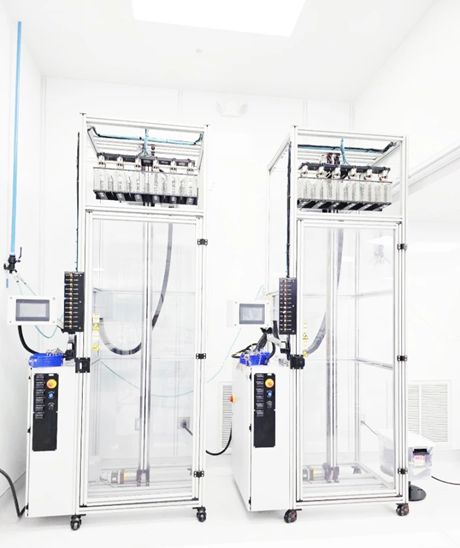
Hydrophilic coatingTwo automated dip-coating systems with programmable draw profiles, plus lamination, reflow and batch curing. Applied and tested on site — removes a vendor, a shipment and a week from every lubricity iteration.2 systems
Laser inspectionAutomated laser inspection for dimensional verification and defect detection, without contact with the device surface.Automated
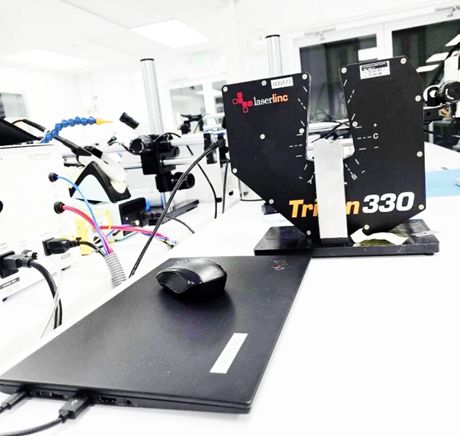
Laser micrometerLaserLinc Triton 330 non-contact laser measurement for outer diameter, ovality and dimensional verification — no contact, no deformation of soft tubing.LaserLinc
Dimensional data captureMeasurement data logged to a workstation for in-process control and records rather than read off a dial and written down.Logged
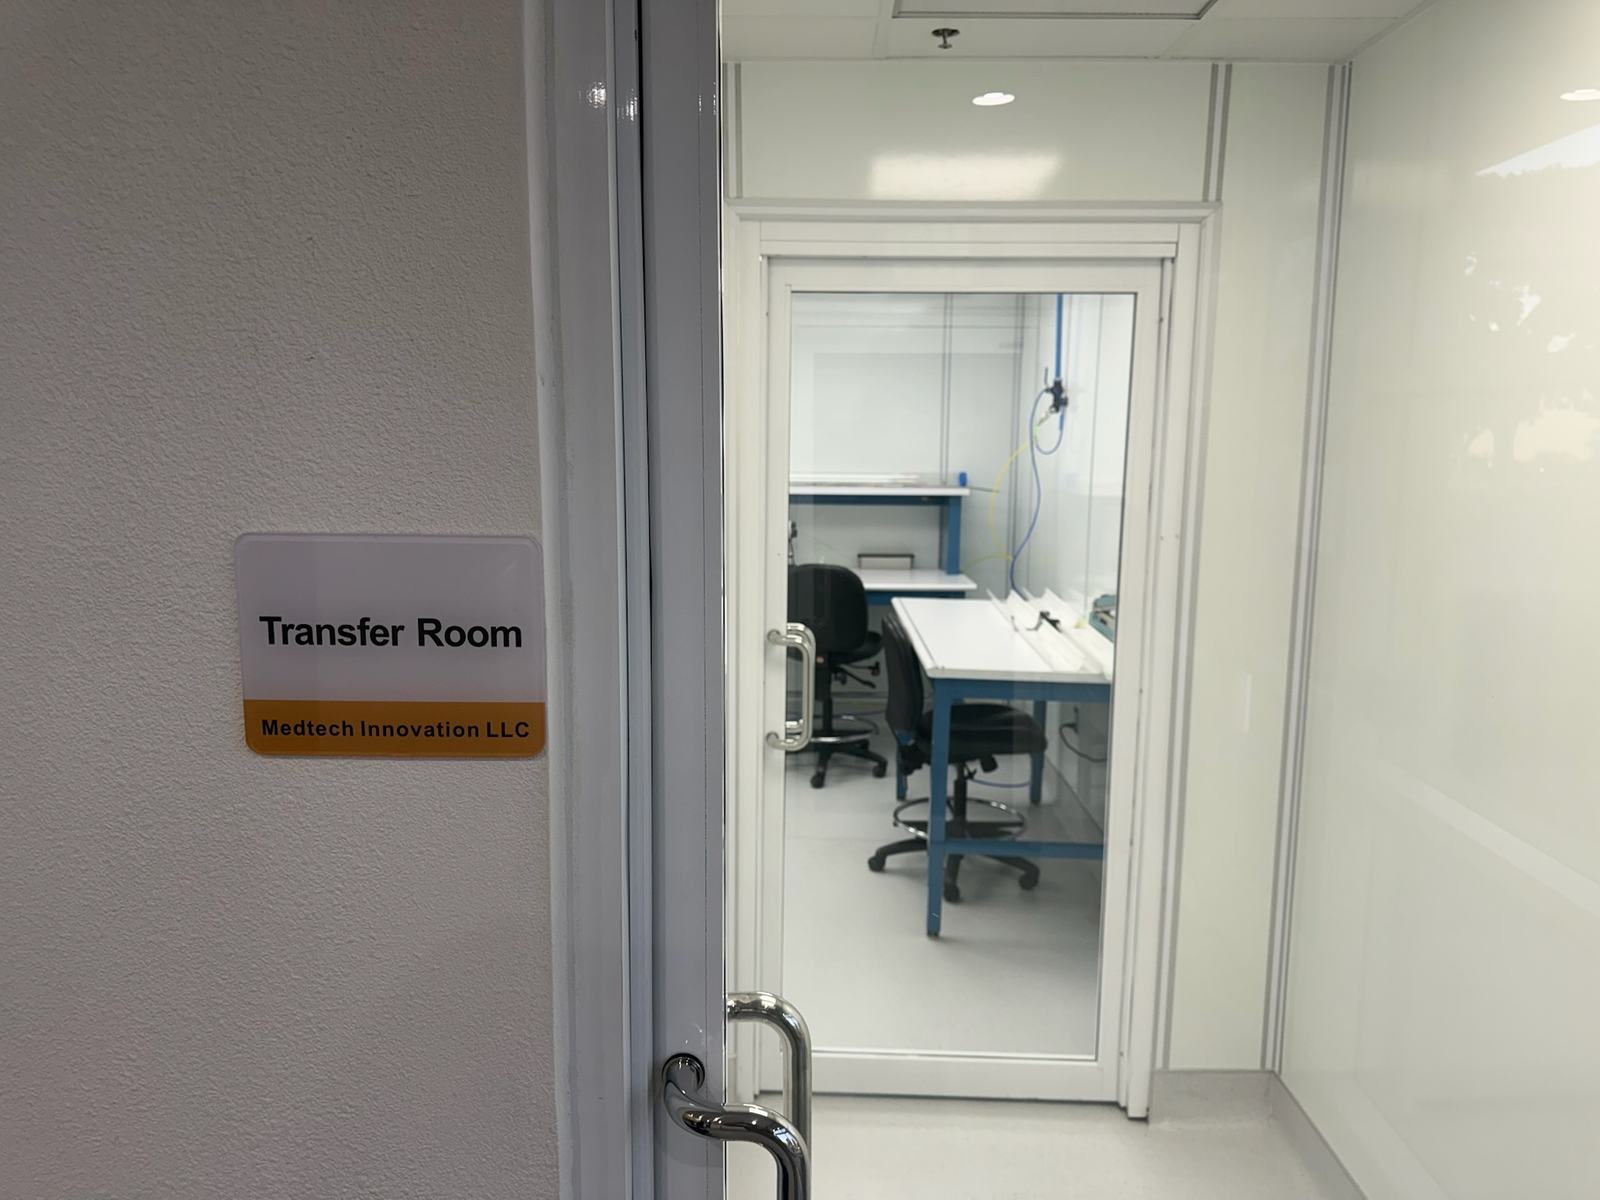
Transfer room airlockMaterials wiped down and unwrapped from shipping packaging before entering the room.Airlock
Gowning & garmentsCoveralls, bouffants, boot covers and gloves, staged and maintained for your team.Provided
Two automated hydrophilic dip-coating towers with touchscreen controls in the cleanroom
Catheter Lamination Equipment
LaserLinc Triton 330 non-contact laser micrometer at a cleanroom bench
Laserlinc – Triton 330 Triple-Axis Micrometer for catheter OD inspection
Long stainless inspection station with laptop showing microcatheter measurement data
Inspection & data capture

03 / Behind the wall

Facility utilities

Supporting infrastructure

Classified space performance depends on supporting infrastructure. Air generation, filtration and pressure control are specified and maintained as an integrated system.

SystemWhat it means for your buildNotes
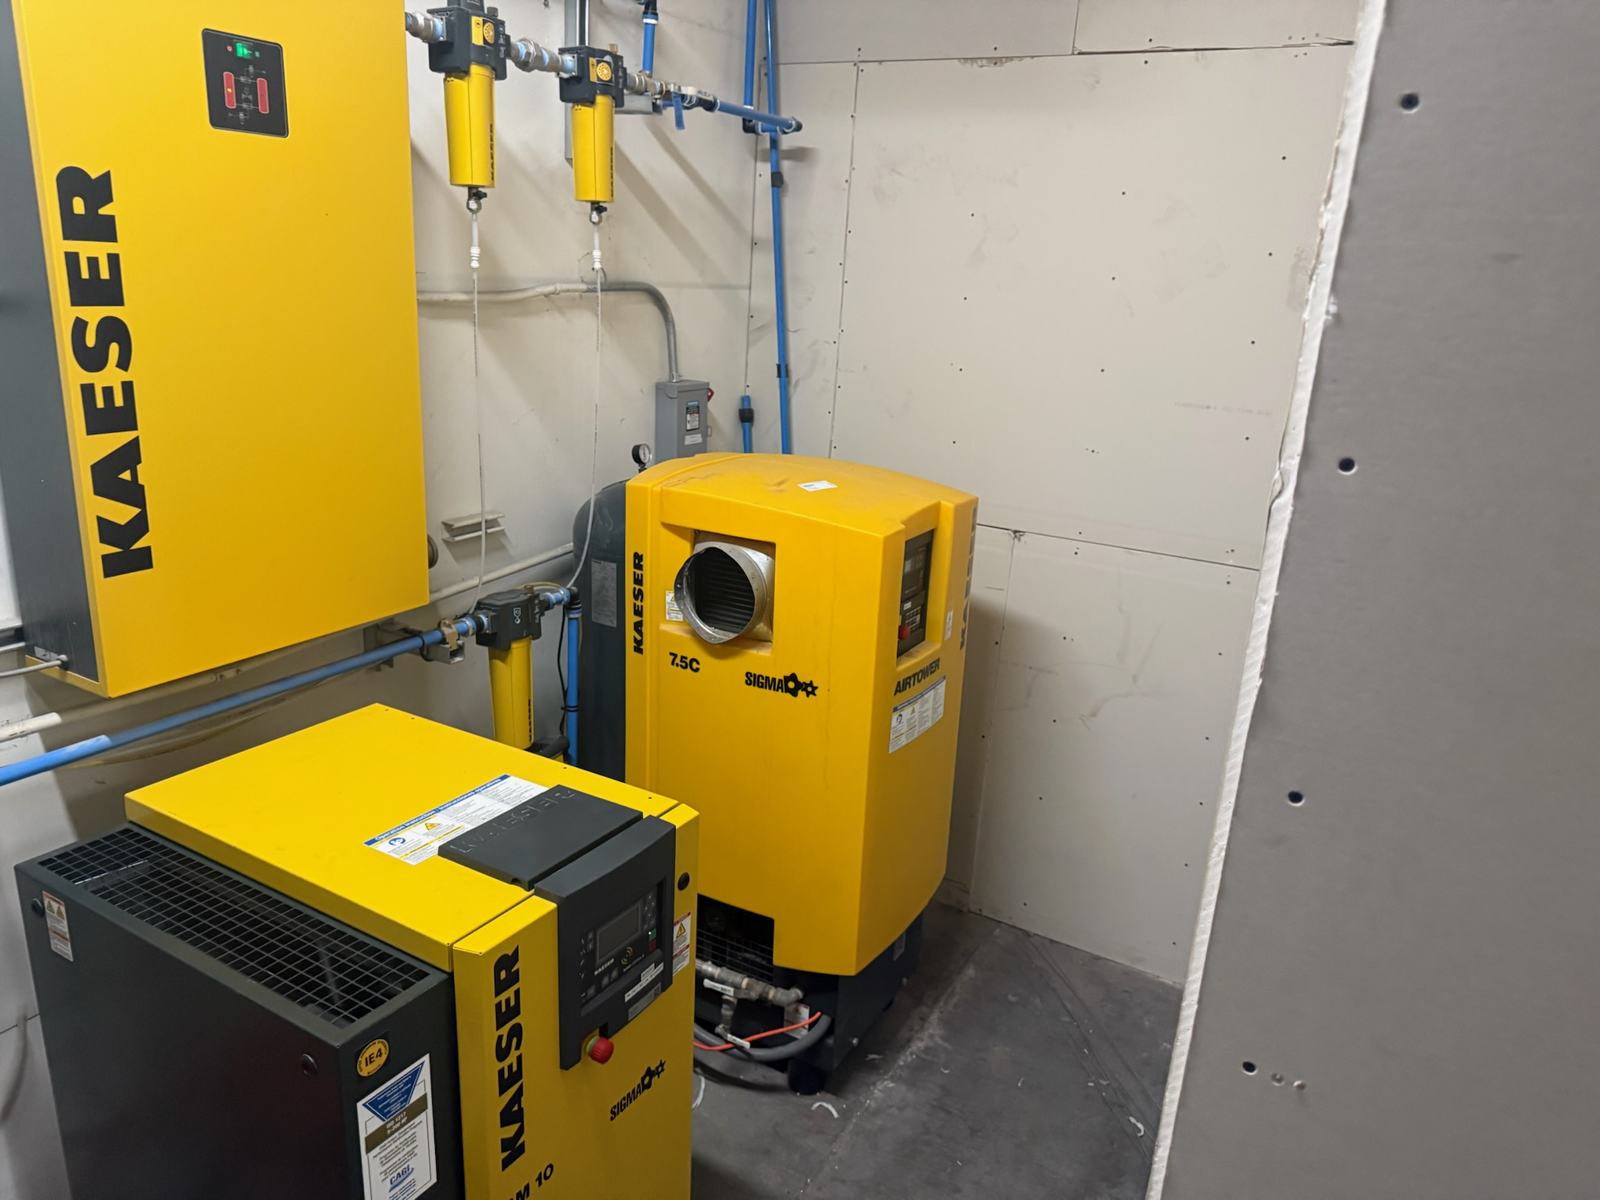
Clean dry compressed airKaeser rotary screw compressor with refrigerated dryer and multi-stage filtration, plumbed to a drop at every bench. Dry, filtered air at the point of use, not shop air off a tank.Kaeser
Hard-wall cleanroom constructionTerra Universal modular panel system with sealed epoxy flooring, vision panels and interlocked doors. Wipeable, non-shedding, and reconfigurable as programs change.Terra Universal
Filtration & pressure cascadeFiltered positive-pressure downflow with a gowning-to-transfer-to-floor pressure sequence, so air always moves from cleaner space toward less clean space.ISO 7
Power at the benchDistributed outlets at every workstation for your dispensers, curing units and test equipment.At bench
Network & access controlStructured cabling, badge-controlled entry and monitored alarm on the facility.Secured
Expansion spaceAdditional classified space available as a program scales, so a successful pilot does not force a vendor change.Available
Kaeser rotary screw compressor and refrigerated air dryer supplying the cleanroom benches
Clean dry air plant
Transfer room airlock with sealing table and bench
Transfer room airlock
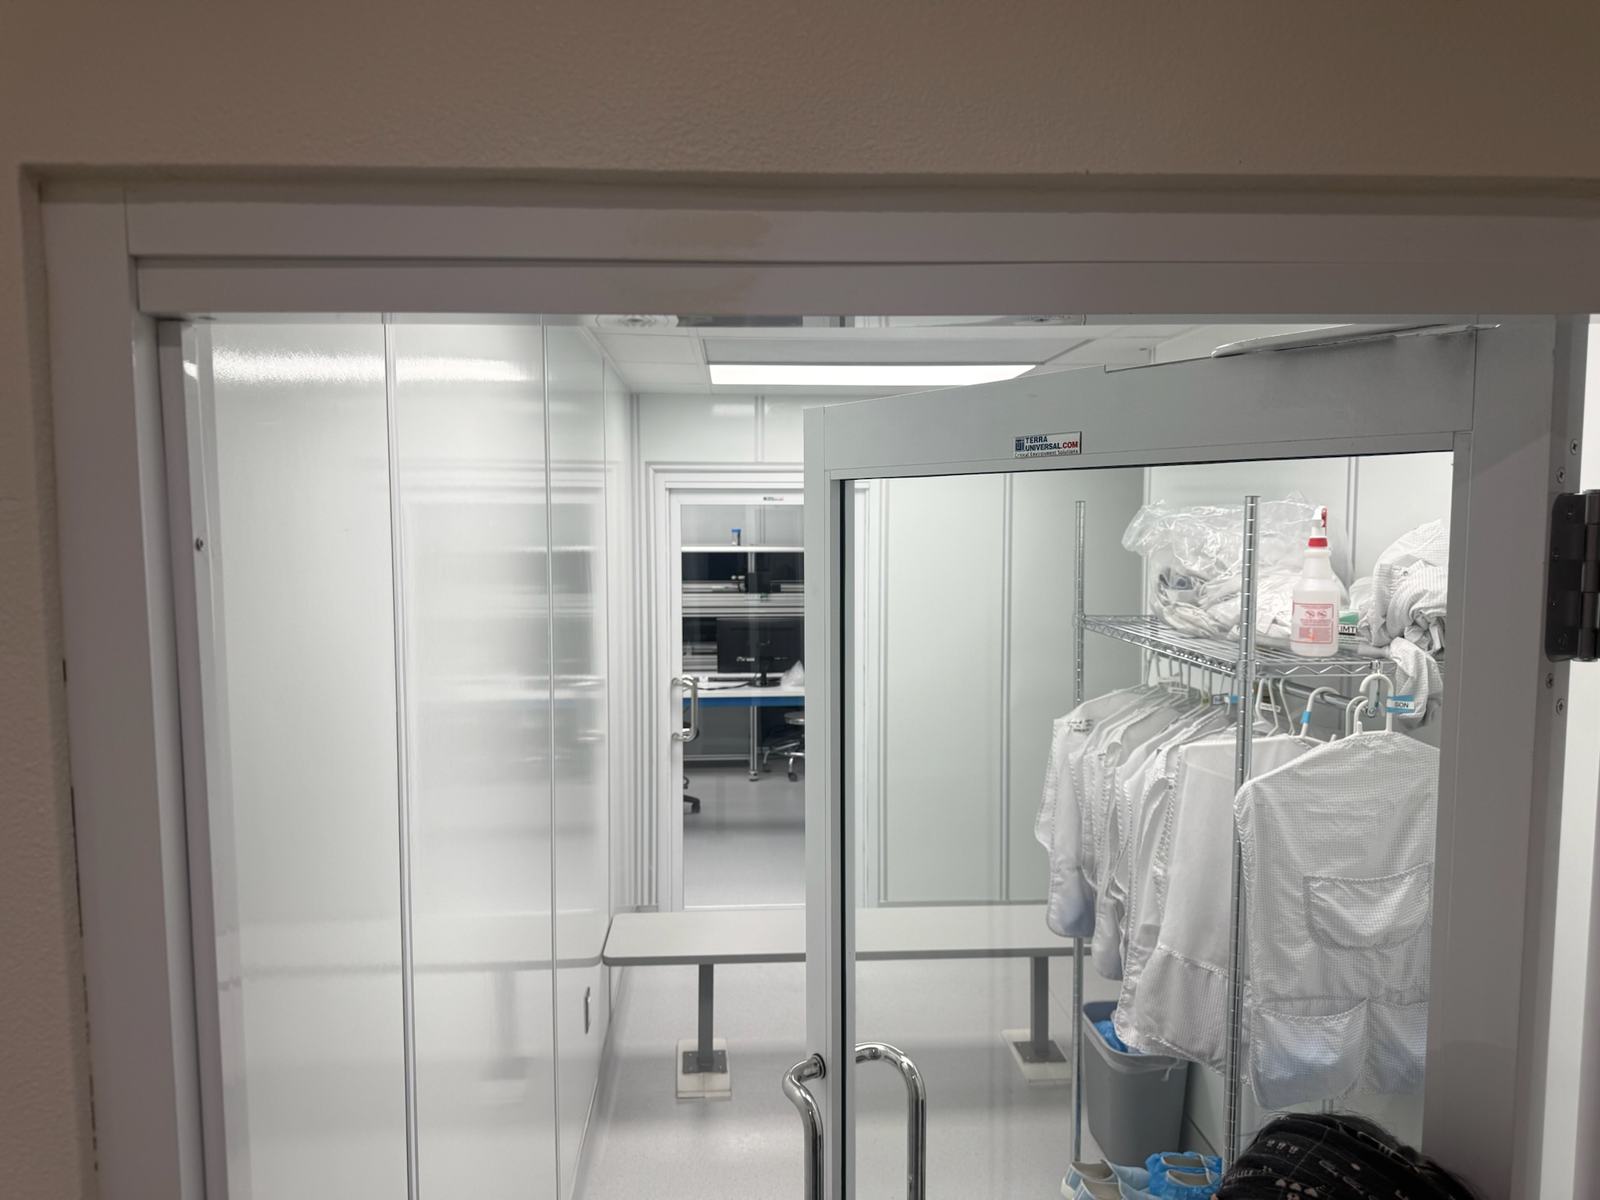
Gowning room with coveralls staged on hangers
Gowning

04 / Before and after the build

Storage, shipping & logistics

Day one is assembly

Material availability is the most common cause of lost schedule at build start. Advance shipment removes it.

ResourceWhat it doesNotes
Advance shippingSend components, fixturing and equipment ahead of your start date. We receive, log and stage everything so your team walks into a ready bench.Pre-start
Receiving & inspectionIncoming materials received and documented against your acceptance criteria, so discrepancies surface before they are built into product.Documented
Secured material storageAssigned storage for incoming components, work in process and finished goods.Assigned
Outbound shippingFinished builds shipped direct to your test lab, sterilizer or clinical site rather than routed back through your office first.Direct
Office desk spaceDesks on site for the engineers who need to sit near the bench, not across town.On site
Records handoverBuild records and materials return to you at the end of the term, whichever team ran the benches.At term end

05 / The resource that is not equipment

Personnel

Available on your program

Build schedule is governed as much by technician qualification and engineering availability as by equipment.

Medical device assembly technicians

Experienced, professional technicians already gowned into this room every day and trained on catheter assembly, bonding, coating and packaging. Available to staff your build under our ISO 13485 quality system, scaled up or down with the schedule.

No recruitment, relocation or training lead time, and no retained headcount after build completion.

Engineering & Technical Support

Experienced engineering and technical personnel support projects from early development through manufacturing, providing senior-level engineering expertise and hands-on implementation support.

  • Product design, feasibility & prototyping
  • Process development & design for manufacturing
  • Tooling, fixtures & equipment implementation
  • Verification, validation & qualification support
  • Design transfer & production launch
  • Manufacturing troubleshooting & process improvement
  • Prototype builds, assembly & technical testing
  • Production setup, documentation & operator support

06 / Honest list

Customer-supplied or sourced per program

Not held on site

Equipment not held on site, identified during scoping rather than at build start.

Not held on site

Some items can be sourced or rented in; others are process-specific and customer-supplied. Submit a process flow for a line-by-line assessment prior to commitment.

  • Tensile testers
  • Flow meters
  • Specialized metrology beyond laser micrometry
  • Program-specific process fixturing and tooling
  • Custom mandrels, dies and forming tools
  • Sterilization — coordinated with third-party providers based on customer requirements
  • Your raw materials, components and packaging stock
  • Validated test methods specific to your device

Manufacturing requirements and limitations are identified during the quotation process, before production begins.

Check your process

Submit a process flow for assessment.

Returned as a line-by-line assessment of on-site capability, customer-supplied requirements and items we can source. Issued in writing prior to commitment.

+1 949-336-2972 [email protected]

17151 Gillette Ave, Irvine, CA — 8 minutes from John Wayne Airport
Mon–Fri, 8:00 AM – 4:30 PM PT

Process inquiries submitted here receive a response by the next business day.